
Company/Organization Profile
The core management team of CECEP Wanrun Co., Ltd. has reviewed and approved the green development goals and action pathways in support of the national dualcarbon strategy, and established a leading group for carbon peaking and carbon neutrality. The company has effectively operated a smart carbon emission management system covering its core businesses. In recent years, it has continuously implemented clean energy replacement and energysaving and carbonreduction technological transformations, and conveyed green and lowcarbon concepts to upstream and downstream partners. The company has displayed its green and lowcarbon work contents and energysaving practice cases on its official website, the official website of Green State Grid and nationallevel associations, and has obtained a number of honors and awards in energy conservation and carbon reduction.
机构简介
中节能万润股份有限公司核心管理团队已审议通过支持国家双碳战略的绿色发展目标与行动路径,成立“碳达峰、碳中和”工作领导小组,有效运行覆盖主营业务的碳排放智慧管理体系;公司近年来持续实施清洁能源替代、节能降碳技术改造,并面向上、下游合作方传递绿色低碳理念,在企业官网、绿色国网官网和国家级协会中展示了绿色低碳工作内容与节能行动案例,并获得了多项节能降碳荣誉与奖项。
Project Overview
Problem Status
The project is carried out in the aircompressor station and production workshops A01, A02 and A03 of CECEP Wanrun Co., Ltd., serving production and utility systems including boiler makeup water preheating, heat preservation of workshop hotwater tanks and plant winter heating. Before implementation, large amounts of lowgrade waste heat from 3040 ℃ circulating water of air compressors, 2530 ℃ workshop circulating water and 50 ℃ cooling circulating water of crystallization kettles were directly discharged and lost through cooling towers. Boiler makeup water, hotwater tank heat preservation and winter heating were heavily dependent on steam heating, resulting in high steam consumption, heavy load of selfproduced steam, prominent contradiction between energy supply and demand, accompanied by thermal pollution and high comprehensive energyuse costs.
Cause Analysis
Although the circulating water contains lowgrade waste heat, its temperature fails to meet the requirement of process heat supply and cannot be directly utilized by ordinary heat exchangers. Wasteheat generation and heatconsumption demands are mismatched due to varying working conditions and seasons. The original mode failed to tap internal wasteheat resources, leading to low energy utilization efficiency.
Improvement Objectives
Adopt heat pump technology and plate heat exchangers to upgrade and recover waste heat from scattered circulating water, adapt to heatusing scenarios such as boiler makeup water, hotwater tanks and heating, reduce thermal emission from cooling towers, cut steam consumption, relieve the pressure on steam supply load, optimize seasonal operation strategies, improve plant energy utilization efficiency, reduce fossilenergy consumption and carbon emissions, and form a recycling mode for lowgrade waste heat in fine chemical industry.
项目背景
问题现状:本项目实施空间为中节能万润股份有限公司厂区空压机站及A01、A02、A03生产车间,服务对象为锅炉补水预热、车间热水槽保温、厂区冬季采暖等生产及公用系统。实施前空压机30-40℃循环水、车间25-30℃循环水、晶化釜50℃降温循环水等大量低品位余热直接经冷却塔排放散失,锅炉补水、热水槽保温、冬季采暖高度依赖蒸汽加热,蒸汽消耗居高不下,自产蒸汽负荷较高,能源供需矛盾突出,同时造成热污染,综合用能成本偏高。
原因分析:循环水含有低品位余热,温度达不到生产用热要求,普通换热器无法直接利用;余热产热与用热需求随工况、季节错配,原有模式未挖掘内部废热资源,能源利用效率较低。
改进目标:依托热泵技术、板式换热器对分散循环水余热提质回收,适配锅炉补水、热水槽、采暖等用热场景,减少冷却塔热排放,降低蒸汽消耗量,缓解蒸汽供应负荷压力,优化分季节运行策略,提升厂区能源利用效率,削减化石能源消耗与碳排放,形成精细化工低品位余热循环利用模式。
Project Implementation
The implementing entity of this project is CECEP Wanrun Co., Ltd., which is jointly promoted by the Equipment Department and production departments. In terms of resource allocation, hightemperature heat pump units and plate heat exchangers are added, the existing circulating water and cooling water pipelines of the plant are utilized, and supporting pipeline connection renovation is carried out. The key project nodes include onsite heat source investigation, working condition parameter collection, multiscenario scheme formulation, zonal renovation construction for aircompressor circulating water and workshop circulating water, commissioning of differentiated operation strategies, system performance verification, and continuous operation and maintenance optimization.
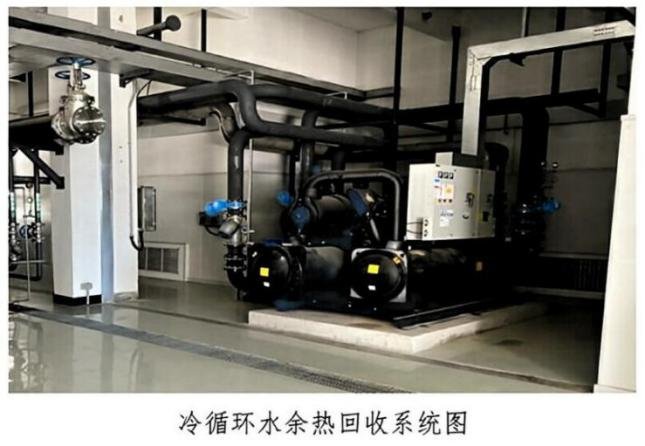
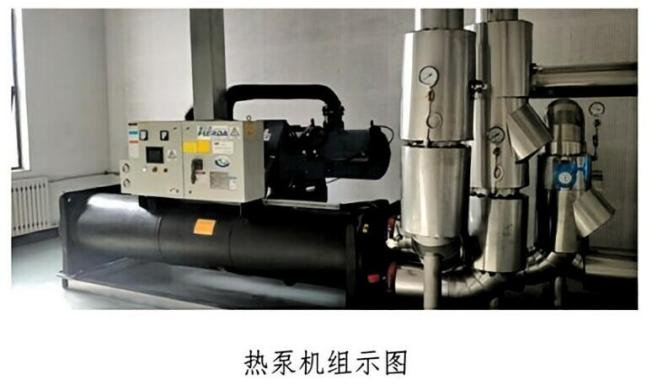
Aiming at the problems that a large amount of 2540 ℃ lowgrade waste heat from circulating water and cooling water in the plant is directly discharged through cooling towers and difficult to be directly utilized due to low heat grade, and the production process is highly dependent on steam heating resulting in large steam consumption, the company carries out systematic energysaving renovation by adopting industrial hightemperature heat pump wasteheat upgrading and recovery technology. Operating based on the reverse Carnot vapor compression cycle, the system relies on closedloop phasechange heat exchange of refrigerant and drives thermal level transition with a small amount of electric power to realize efficient collection, upgrading and reuse of lowgrade waste heat: the lowtemperature and lowpressure refrigerant absorbs lowtemperature waste heat from plant circulating water and cooling water and vaporizes in the evaporator, and becomes hightemperature and highpressure gaseous refrigerant after adiabatic compression by the compressor to complete heat grade upgrading, converting originally unavailable lowtemperature waste heat into usable process heat source. Heat is then released to heating circulating water, boiler makeup water and workshop hotwater tanks through the condenser. The highpressure refrigerant after heat release and temperature reduction is depressurized and cooled by the throttling device and reenters the evaporator for continuous circulation, forming a continuous and stable heat transfer and upgrading process.
The project makes full use of the existing plant pipe network, installs additional hightemperature heat pump units and plate heat exchangers, and implements multiscenario and differentiated operation strategies in combination with plant working conditions. For the direct discharge of cooling water waste heat in the aircompressor station and its low heat grade for direct utilization, heat pump wasteheat recovery technology is adopted to recover lowgrade waste heat from aircompressor station cooling water, heating winter heating water to 50 ℃ in the heating season, and raising the temperature of boiler makeup water from 25 ℃ to 5062 ℃ in the nonheating season.
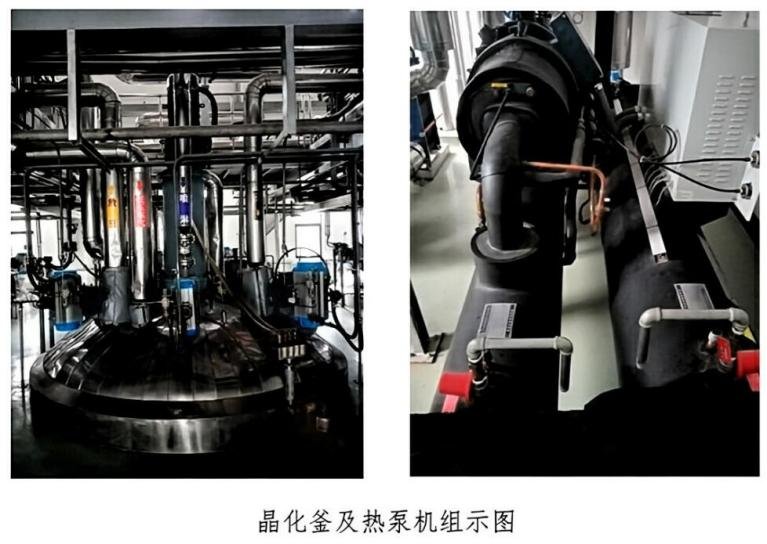
To address high steam consumption for heat preservation of workshop hotwater tanks and waste of lowtemperature waste heat from crystallization kettle cooling water, the combined process of preheating by frontmounted heat exchangers plus heatsupplementing by endofline heat pump upgrading is adopted to recover lowtemperature waste heat nearby to replace steam heat sources for hotwater tank heat preservation.
The energy management platform is applied to collect operating data in real time and dynamically optimize unit output power and operation duration, so as to solve efficiency attenuation caused by timesequence mismatch between wasteheat supply and demand and workingcondition fluctuation. Meanwhile, a standardized special operation and maintenance system is established to ensure longterm efficient and stable system operation through regular inspection, parameter control, post training and ledger management.
Upon project completion, the aircompressor circulating water system saves 12,890 tons of steam annually and the workshop saves 12,569 tons of steam per year. Largescale upgrading and reuse of lowgrade waste heat is realized, providing a referable implementation example for lowtemperature circulating water wasteheat recovery in the fine chemical industry.
项目实施
本项目实施主体为中节能万润股份有限公司,由设备部、生产部门协同推进,资源配置上增设高温热泵机组、板式换热器,利旧厂区原有循环水、冷却水管道,配套建设管路对接改造,项目关键节点包含现场热源摸排、工况参数采集、多场景方案编制、空压机循环水、车间循环水分区域改造施工、差异化运行策略调试、系统性能核验、持续运维优化。
针对厂区内大量25-40℃低品位循环水、冷却水余热经冷却塔直接排放、热能品味较低难以直接利用,生产环节高度依赖蒸汽加热导致蒸汽消耗量大的问题,公司采用工业高温热泵余热提质回收技术开展系统性节能改造。该系统基于逆卡诺蒸汽压缩循环运行,通过冷媒闭环相变换热,以少量电能驱动热力层级跃迁,实现低品位废热的高效采集、提质与回用:低温低压冷媒在蒸发器内吸收厂区循环水、冷却水的低温余热并汽化,经压缩机绝热压缩后形成高温高压气态冷媒,完成热能能级提升,将原本无法利用的低温余热升级为生产可用热源,再通过冷凝器向采暖循环水、锅炉补水、车间热水槽供水释放热量,放热降温后的高压冷媒经节流装置降压降温,重新进入蒸发器持续循环,形成连续稳定的热量搬运与提质过程。
项目充分利旧厂区原有管网,配套新增高温热泵机组与板式换热器,结合厂区工况实行分场景、差异化运行策略。针对空压站冷却水余热直排、热能品位低难以直接利用的问题,通过热泵余热回收技术回收空压站冷却水低品位余热,在采暖季将冬季采暖水升温至50℃;在非采暖季将锅炉补水温度由25℃提升至50-62℃。
针对车间热水槽保温耗蒸汽量大、晶化釜冷却水低温余热浪费问题,通过换热器前置预热+热泵末端提质补热的组合工艺,就近回收低温余热替代蒸汽热源,实现热水槽保温。
依托能源管理平台实时采集运行数据,动态优化机组输出功率与运行时长,解决余热供需时序错配、工况波动导致的效率衰减问题。同步建立标准化专项运维体系,通过常态化巡检、参数管控、岗位培训及台账管理,保障系统长期高效稳定运行。
项目完成后空压机循环水系统年节约蒸汽12890吨,车间年节约蒸汽12569吨,实现低品位余热规模化提质回用,为精细化工行业低温循环水余热回收提供可借鉴的实施范例。
Project Outcome
A distinct quantitative comparison can be drawn before and after project implementation. Before renovation, the waste heat of lowtemperature circulating water from the aircompressor station and Workshops A01, A02 and A03 of CECEP Wanrun Co., Ltd. was discharged into the atmosphere through cooling towers. Boiler makeup water, hotwater tank heat preservation and plant heating relied on steam supply, imposing a heavy steamgenerating load on boilers. After the completion of renovation, the aircompressor circulating water system saves 12,890 tons of steam annually; Workshop A01 and Workshop A02 save 4,050 tons of steam per year, and Workshop A03 saves 8,519 tons of steam annually. The total annual steam saving reaches 25,459 tons, which greatly eases the contradiction between steam supply and demand and reduces useless heat dissipation of the plant to improve the plant thermal environment. Meanwhile, the energy management platform realizes visualization of energyconsumption data and significantly improves the efficiency of refined energy management.
The project boasts multiple innovation highlights. In terms of technological innovation, heat pump units are adopted to upgrade lowgrade waste heat of circulating water, and plate heat exchangers are combined to realize cascade utilization of heat, breaking the technical bottleneck that lowtemperature waste heat cannot be reused due to insufficient temperature. In terms of model innovation, a differentiated seasonal operation strategy is explored: waste heat is preferentially used for plant heating in winter and for preheating boiler makeup water in nonheating seasons to adapt to seasonal fluctuations in energy consumption.
In addition, the project features favorable sustainability and replicability. Based on the original equipment operation and maintenance mechanism, a longterm operation mechanism for data review and dynamic optimization of working conditions is established. Routine team inspections, regular heat exchanger cleaning and heatpump unit maintenance, onthejob practical training and complete operation ledger filing are implemented without additional fulltime staff. The economic benefits generated by the project cover equipment power consumption and operationmaintenance costs to achieve economic selfsustainability. Making full use of the existing circulating water pipe network and taking heatpump wasteheat recovery as the core, the project is applicable not only to the fine chemical industry but also to buildingmaterial, food and other industries with massive coolingwater wasteheat discharge. It can be implemented simply by finetuning equipment configuration according to each enterprise’s heatsource flow rate and heatconsumption load, providing a mature and promotable practical sample for wasteheat recovery of industrial enterprises.
成果亮点
项目实施前后形成鲜明量化对比,改造前,中节能万润股份有限公司空压机站、A01、A02、A03车间低温循环水余热经冷却塔被排放至大气中,锅炉补水、热水槽保温、厂区采暖依靠蒸汽供热,锅炉产蒸汽负荷较高。改造完成后,空压机循环水系统年节约蒸汽12890吨,A01车间、A02车间年节约蒸汽4050吨,A03车间年节约蒸汽8519吨,合计年节省蒸汽25459吨,大幅缓解蒸汽供需矛盾,同时减少厂区无效热散逸,改善厂区热环境。同时,借助能源管理平台实现能耗数据可视化,能源精细化管理效率显著提升。
项目拥有多项创新亮点,技术创新上采用热泵机组对低品位循环水余热提质,结合板式换热器实现热量梯级利用,破解低温余热温度不足难以回用的技术瓶颈;模式创新上探索季节差异化运行策略,冬季余热优先保障厂区采暖,非采暖季用于锅炉补水预热,适配用能的季节性波动。
同时,该项目具备良好持续性与可复制性,依托原有设备运维机制建立数据复盘、工况动态调优的长效运行机制,落实班组日常巡检,定期清洗换热器、维护热泵机组,开展岗位实操培训,完整留存运行台账,无需增设专职人员。项目产生的经济效益覆盖设备耗电及运维成本,实现经济自维持;充分利旧原有循环水管网,以热泵余热回收为核心,除精细化工外,还可适配建材、食品等存在大量冷却水废热排放的行业,只需按照各企业热源流量、用热负荷微调设备配置即可落地,为工业企业余热回收提供成熟可推广的实践样本。
Project Highlights
The statistical and accounting time scope of this project is based on 300 operating days per year with 24hour continuous production. The accounting boundary covers the waste heat recovery and renovation system of the aircompressor station and Workshops A01, A02 and A03 in the plant of CECEP Wanrun Co., Ltd. In terms of ecological and environmental benefits, the project saves 25,459 tons of steam annually, equivalent to 2,189 tons of standard coal, and reduces carbon dioxide emissions by 7,637 tons per year. It mitigates plant thermal pollution caused by direct wasteheat discharge from cooling towers and cuts fossil energy consumption. Meanwhile, cost reduction and efficiency improvement are achieved with an approximate annual comprehensive cost saving of RMB 7.63 million. From the perspective of social impact, jointly promoted by the Production Department and Equipment Department, the project fosters a strong corporate atmosphere for energy conservation. It has won honors including the First Prize of Shandong Provincial Equipment Management Innovation Achievements and the First Prize of Equipment Management and Technological Innovation Achievements issued by the China Association of Plant Engineering. As a typical case of scientific and technological innovation for dualcarbon goals, it provides a replicable demonstration for upgrading and recovery of lowgrade waste heat in fine chemical, buildingmaterial, food and other industries.
成果影响力
本项目统计核算时间范围按年运行300天、24小时连续生产,边界为中节能万润厂区空压机站、A01、A02、A03车间余热回收改造系统。生态环境效益方面,项目年节约蒸汽2545吨,折合节约标准煤2189吨,年减少二氧化碳排放7637吨,减少冷却塔余热直排带来的厂区热污染,降低化石能源消耗;同时实现降本增效,综合年节约费用约763万元。社会影响层面,项目依托生产部、设备部协同推进,营造了浓厚的企业节能氛围,该项目还获得山东省设备管理创新成果一等奖、中国设备管理协会设备管理与技术创新成果一等奖等荣誉,作为双碳科技创新典型案例,为精细化工及建材、食品等行业低品位余热提质回收提供可复制示范案例。
Reviews & Honors
In terms of evaluation and feedback, according to feedback from the Production Department and verification by the Equipment Department, the renovated system operates stably, the wasteheat upgrading effect meets the design expectation, and steam consumption is effectively reduced. Onsite verification by a thirdparty energysaving service provider confirms that all energy consumption and carbon reduction indicators have met the standards. This project practice is included in the green and lowcarbon practice section of the listed company’s ESG report, and provides important support for the obtained nationallevel green factory construction. In terms of media and industry recognition, the project case has been publicly published and promoted on the platform of the Special Committee for Carbon Peaking and Carbon Neutrality of China Association of Plant Engineering. Shared externally as a typical practice of lowgrade waste heat recovery in fine chemical industry, it offers reference for enterprises in the same industry. In terms of awards and honors, after the implementation of this wasteheat recovery and reuse system project, Wanrun Company has been rated as an advanced unit in annual energysaving work, and won the First Prize of Equipment Management and Technological Innovation Achievements issued by China Association of Plant Engineering, the First Prize of Shandong Provincial Equipment Management Innovation Achievements, and the Typical Case of DualCarbon Scientific and Technological Innovation. Relevant achievements have obtained phased recognition from local competent energysaving authorities, delivering a replicable practical case for industrial wasteheat recovery renovation.
评价与荣誉
评价反馈方面,经生产部门反馈及设备部核验,系统改造后运行稳定,余热提质效果达到设计预期,有效降低蒸汽消耗;第三方节能服务商现场核验确认各项能耗、减碳指标达标,该项目实践纳入上市公司ESG报告绿色低碳实践板块,为已获得的国家级绿色工厂建设提供重要支撑。媒体/行业认可方面,项目案例被中国设备管理协会碳达峰碳中和专委会平台公开刊载推介,作为精细化工低品位余热回收典型实践对外分享,为同行业企业提供参考借鉴。奖项荣誉方面,该余热回收再利用系统项目实施后,万润公司获评年度节能工作先进单位,斩获中国设备管理协会设备管理与技术创新成果一等奖、山东省设备管理创新成果一等奖、双碳科技创新典型案例,相关成果获得地方节能主管部门的阶段性认可,为工业余热回收改造提供可复制的实践案例。
近零碳社区的美育升级---- 长寿苑社区 “低碳实践 + 影像科普” 共建项目
4天前 · 来源:成都市武侯区火车南站街道长寿苑社区居民委员会 · 作者:成都市武侯区火车南站街道长寿苑社区居民委员会
以绿色金融之力推动中国新质生产力!
4天前 · 来源:国泰海通证券研究所ESG及美丽中国研究组 · 作者:国泰海通证券研究所ESG及美丽中国研究组
不择知行细流,蕴蓄蓝绿成深:雄安新区生态环境共享中心科普宣传空间营造雄安新区生态环境共享中心VR虚拟实验室(数字化仿真替代实体化学实验,实现科普零危废、低能耗)
6天前 · 来源:雄安新区生态环境监控中心 · 作者:雄安新区生态环境监控中心
